
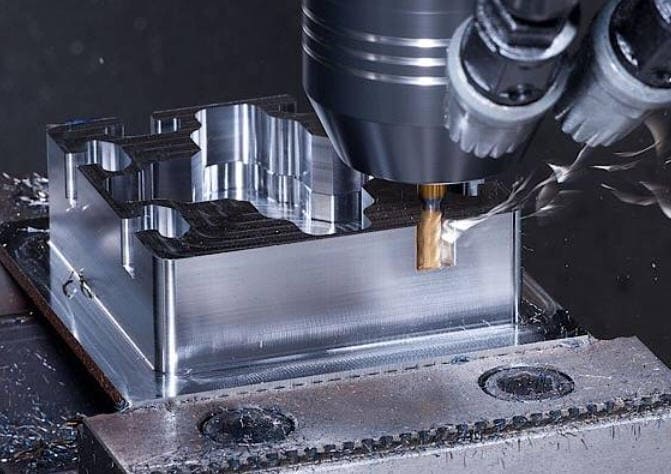
Four ways an aluminum part goes out of spec — and what we do about each
Aluminum rarely fails because the cutter could not remove the material. It fails because the material moved: during roughing, during clamping, during aging, or during coating. These are the four we plan around before the first chip.
The block bows after roughing
Rolled and heat-treated plate carries locked-in stress from quenching. Remove 70% of the mass and that stress rebalances — a plate that was flat in the saw cut comes off the machine with 0.3 mm of bow. 7075-T6 and thick 6061-T651 plate are the worst offenders, and the part usually passes first-article inspection before relaxing overnight.
Thin walls push away from the cutter
A 1 mm wall deflects under side load, so the cutter takes less than the programmed depth and the wall ends up thick, tapered, or chattered. Clamping is just as dangerous: a vise closing on a thin-wall frame prints its own distortion into the finished dimensions.
The bore fits before anodizing, not after
Anodizing is conversion, not plating: roughly half the coating thickness grows outward from the original surface. A 25 µm hard anodize adds about 12 µm per surface — around 0.025 mm on a diameter. Bearing bores, dowel holes and sliding fits that were dead-on as-machined become interference fits after Type III.
Soft alloys smear instead of cutting
5052, 6063 and 1100 are gummy. Aluminum welds to the cutting edge, then breaks away and tears the surface — you get a torn Ra 6.3 finish where the drawing asked for 1.6, galled threads, and burrs that hand-deburring cannot fully remove from an internal corner.
Where the tolerance actually goes on a stress-prone aluminum part
For a straightforward bracket we run a conventional route. For thin walls, thick plate, 7075, or any part with a flatness or true-position callout under 0.05 mm, the job goes down this six-stage route instead. It costs more setups. It is the reason the parts stay in spec three weeks after they land.

Material & certs
Alloy and temper verified against the mill certificate before cutting. Substitutions never happen silently.
Stress relief
Pre-machining anneal on high-risk plate and 7075 so the bulk stress is released off the machine.
Symmetric roughing
Balanced material removal, 0.3–0.5 mm left everywhere, then a rest period to let the part settle.
Re-fixture
Vacuum plate or soft jaws cut to the part's own profile. Clamping load spread, never concentrated.
Finish to pre-plate size
Final passes cut to the compensated dimension when a coating is specified, not the drawing nominal.
Post-coat verification
Critical features re-measured on the CMM after surface treatment — the dimension you actually receive.
Stage 02 and Stage 06 are the two most shops skip. They are also the two that decide whether a precision aluminum part passes incoming inspection at your end.
The aluminum alloys we machine — and how each one behaves in the cut
Datasheets tell you tensile strength. They do not tell you which alloy will chatter on a thin rib, which one will smear a thread, or which one anodizes to a consistent black. This table is written from the machine side.
| Alloy | Typical temper | Behavior in the cut | Best suited to | Anodizing response |
|---|---|---|---|---|
| 6061 | T6 / T651 | The default benchmark. Predictable chips, clean threads, good finish. T651 plate carries meaningful residual stress on thin sections. | General structural parts, housings, brackets, plates, fixtures | Excellent, clear and Type II color; consistent |
| 6082 | T6 / T651 | Machines almost identically to 6061, marginally stronger in thick plate. Slightly duller as-machined face. | EN-standard drawings, European supply chains, structural plate | Good; very close to 6061 |
| 6063 | T5 / T6 | Softer and gummier than 6061 — prone to built-up edge on finishing passes and burr formation at exits. | Extruded profiles machined to length, enclosures, trim, heat-sink bodies | Excellent — the standard choice for decorative anodizing |
| 5052 | H32 | Non-heat-treatable and notably gummy. Needs sharp uncoated tooling and aggressive chip load to avoid smearing. | Marine and outdoor parts, formed sheet components, fluid contact parts | Good clear anodize; color can vary batch to batch |
| 5083 | H111 | Tough and stringy; long chips need managed evacuation. Best corrosion resistance in the group, weldable. | Marine hardware, cryogenic and pressure vessel components, weldments | Acceptable clear; not recommended for cosmetic color |
| 7075 | T6 / T651 | Steel-adjacent strength with good machinability, but the most stress-prone alloy we run. Thin walls and asymmetric pockets require staged roughing without exception. | Aerospace structure, high-load brackets, mold plates, tooling | Type II and Type III both viable; color runs darker and less even than 6061 |
| 7050 | T7451 | Similar to 7075 with better stress-corrosion behavior in thick sections; the preferred choice when 7075 plate is too unstable. | Thick aerospace structure, high-strength machined plate | Comparable to 7075 |
| 2024 | T351 | Machines cleanly with excellent chip control and strong fatigue performance. Poor corrosion resistance — needs a coating in almost every application. | Aircraft fittings, fatigue-loaded structure, precision shafts | Requires anodize or chem-film for corrosion protection |
| 2017A | T4 | Free-machining behavior close to 2011; excellent for high-volume turned parts with fine threads. | Turned fittings, connectors, threaded inserts | Poor cosmetic result; specify chem-film instead |
| MIC-6 / ATP-5 | Cast plate | Cast and stress-relieved specifically for stability — essentially no residual stress, so it stays flat through heavy material removal. Softer and more porous than wrought. | Fixture plates, jigs, base plates, optical and inspection tooling | Uneven and porous — anodize only for protection, never cosmetics |
Not sure which alloy to specify? Send the drawing and the load case — our engineers will recommend one and tell you what it costs against your current callout. Deeper reading: our guide to the aluminum CNC machining process.
We pick the machine around your part, not the other way round
Aluminum is machined on every one of our platforms. The right route depends on geometry, setup count and how much of your tolerance budget you can afford to spend on re-fixturing.

CNC milling
Plates, covers, manifold bodies, brackets and enclosures. The workhorse route for prismatic aluminum parts and the most cost-effective at any volume.

5-axis machining
Angled faces, undercuts and organic surfaces in one setup. Fewer setups means fewer re-fixturing errors — the single biggest source of true-position drift on complex housings.

CNC turning
Shafts, spacers, bushings, adapters and flanged bodies. Live tooling handles cross-holes and flats without a second machine.

Turn-mill machining
Rotational parts with milled features completed in one clamping. Concentricity between turned and milled features holds because the part never leaves the spindle.

Swiss aluminum machining
Small-diameter, long-aspect aluminum parts — pins, contacts, micro shafts. Guide-bushing support keeps slender aluminum from whipping.

Wire EDM
Sharp internal corners and thin profiles a cutter cannot reach, with zero cutting force — useful on features that would otherwise deflect.
What we hold, and what it costs you to ask for it
Tolerance is a budget, not a badge. We can hold ±0.005 mm — on a specific feature, in a specific setup, with in-process gauging. Applying that number to every dimension on the drawing multiplies your unit price for no functional gain. Below is what each band actually means in production.
| Characteristic | Standard (default) | Precision (on request) | Notes |
|---|---|---|---|
| Linear dimensions | ISO 2768-m | ISO 2768-f / ±0.01 mm | Applied to all untoleranced dimensions unless your title block states otherwise |
| Critical features | ±0.02 mm | ±0.005 mm | Per-feature, with dedicated setup and in-process measurement; call these out explicitly |
| Hole diameter | H8 | H7 (reamed / bored) | H7 and tighter needs a reaming or boring operation — flag bearing and dowel bores |
| Flatness, ≤200 mm plate | 0.1 mm | 0.03 mm | Tighter than 0.05 mm on wrought plate normally requires stress relief or a switch to MIC-6 |
| Concentricity, turned | 0.05 mm TIR | 0.01 mm TIR | Precision band requires single-setup turn-mill or Swiss machining |
| Surface finish, as-machined | Ra 3.2 µm | Ra 0.8 µm | Ra 0.4 µm and below on aluminum needs polishing or diamond turning — ask before specifying |
| Angular | ±0.5° | ±0.1° | 5-axis single setup recommended for the precision band |
All final dimensions verified on coordinate measuring machines. Dimensional reports are supplied with every shipment; full first-article and PPAP documentation is available on request.
Finishes, and exactly what each one does to your dimensions
Most finishing tables list appearance and corrosion resistance. The column that causes rejected parts is the dimensional one — so we put it first.

| Finish | Typical thickness | Dimensional change | Why you would specify it |
|---|---|---|---|
| As-machined | — | None | Lowest cost; tool marks visible. Fine for internal and non-cosmetic parts |
| Bead blasting | — | ≈0.01 mm removal | Uniform matte texture; removes tool witness marks before anodizing |
| Anodizing Type II | 5–25 µm | ≈ +½ of thickness per surface | Corrosion resistance plus color. The default for visible aluminum parts |
| Hard anodizing Type III | 25–50 µm | ≈ +12–25 µm per surface | Wear surfaces, sliding fits, pneumatic bores. Mask or pre-compensate critical features |
| Chem film / chromate | <1 µm | Negligible | Corrosion protection that keeps the surface electrically conductive — grounding and RF parts |
| Powder coating | 60–120 µm | Substantial — mask all fits | Durable colored finish for enclosures and exterior housings |
| Electroless nickel | 5–25 µm | + full thickness per surface | Hardness and wear resistance with uniform coverage into bores and blind features |
| Brushing / polishing | — | 0.01–0.05 mm removal | Cosmetic grain or mirror faces; usually followed by clear anodize |
| Laser marking | — | None | Permanent part numbers, logos, traceability codes and date coding |
Tell us the coating class on the drawing and we will machine to the pre-plate dimension. If the drawing is silent, we ask — we do not guess.
Design rules that take cost out of an aluminum part
Roughly 60–70% of the price of a machined aluminum part is decided by the model, not the quotation. These are the five changes that move the number most, and the limits we work to.

| Feature | Recommended | Achievable |
|---|---|---|
| Wall thickness | 1.5 mm | 0.8 mm |
| Internal corner radius | ≥ ⅓ cavity depth | R0.5 mm |
| Pocket depth / tool dia. | 4 : 1 | 10 : 1 |
| Hole depth / diameter | 4 : 1 | 10 : 1 |
| Minimum hole diameter | 1.0 mm | 0.3 mm |
| Thread depth | 2× diameter | 3× diameter |
| Engraved text height | 2.0 mm | 0.5 mm |
| Boss / rib aspect ratio | 3 : 1 | 8 : 1 (supported) |
Five changes that reliably cut the price
- Round your internal corners generously. A cavity with R1 corners forces a 2 mm cutter and a slow feed. Opening the same corners to R3 lets us run a 6 mm tool at four times the material removal rate.
- Tolerance only what mates. Give the bearing bore ±0.01 mm and let the outer profile sit at ISO 2768-m. Blanket-tight drawings add inspection time to every feature.
- Keep deep pockets shallow where you can. Beyond about 4× tool diameter we switch to longer, more flexible tooling with lighter cuts — the same pocket takes two to three times longer.
- Design for fewer setups. Every feature that requires a sixth face adds a setup, a fixture and a stack-up error. Consolidating onto five faces often removes a whole operation.
- Say what the surface has to do. "Ra 0.8, cosmetic" and "Ra 0.8, sealing face" are different parts. Tell us which, and we will finish the one that matters and leave the other as-machined.
Send a STEP file and we will return a marked-up DFM report with the cost drivers identified — free, and before you commit to anything.
Request a DFM reviewAluminum parts we machine every week
Different industries stress different failure modes. What changes between them is not the alloy — it is which tolerance you cannot afford to lose.

Aerospace
7075 and 2024 structure where stress relief and full material traceability are non-negotiable.
Brackets · ribs · housings · fittings
Robotics & automation
Lightweight 6061 and 7075 structure where mass at the end of an arm directly costs payload.
Joint housings · arm links · end-effector mounts
Thermal management
High-fin-density 6061 and 6063 heat sinks, including cold plates for AI server racks.
Heat sinks · cold plates · manifold bodies
Automotive & EV
Battery housings, sensor brackets and prototype-to-production transitions on the same tooling.
Enclosures · brackets · fluid blocks
Medical devices
Anodized 6061 instrument bodies and imaging frames with documented finishing processes.
Housings · frames · positioning components
Tooling & fixtures
MIC-6 cast plate fixtures and tooling plates that stay flat through heavy pocketing.
Fixture plates · jigs · inspection basesWhat arrives with the parts
Every aluminum order ships with the paperwork your incoming inspection needs, because a part with no evidence behind it is a part your QA team has to re-measure from scratch.
- Material certificate — mill test report identifying alloy, temper and heat lot
- Dimensional report — CMM results against your drawing's critical characteristics
- First-article inspection — full FAI or PPAP documentation on request for production programs
- In-process control — first-piece, in-process and final inspection under our ISO 9001:2015 system
- Post-coating verification — critical features re-measured after surface treatment, not before
- Production visibility — MES tracking so you can see order status at any stage
 Volume & lead time
From one part to a hundred thousand
We do not run a prototype shop and a production shop as separate businesses, which is what usually forces you to re-qualify a supplier at the worst possible moment.
| Stage | Quantity | Typical lead time |
|---|---|---|
| Prototype | 1–10 | 7–10 days |
| Bridge / pilot | 10–500 | 10–20 days |
| Production | 500–100,000+ | Scheduled release |
Lead times depend on finish, alloy availability and inspection scope — confirmed with your quotation. No minimum order quantity.
From drawing to delivered parts
Four stages, one engineer as your point of contact throughout.

Send your files
STEP or IGES plus a dimensioned PDF. NDA in place first if you need one.
Quote & DFM
Price, lead time and a marked-up manufacturability review within two working hours.
Machining & inspection
Production under ISO 9001:2015 control, with first-piece approval before the run continues.
Finishing & shipping
Surface treatment, post-coat verification, protective packing and worldwide delivery.
What to include in your RFQ
- 3D model (STEP / IGES / X_T / SLDPRT)
- 2D drawing with tolerances and datums
- Alloy and temper, or the application if you want a recommendation
- Which features are critical, and why
- Surface finish and coating class
- Whether coated dimensions are before or after plating
- Quantity now, and expected annual volume
- Required certifications or inspection documentation
Aluminum CNC machining questions
Which aluminum alloy should I choose for CNC machining?
6061-T6 is the correct default for around 70% of machined parts — it balances strength, machinability, corrosion resistance and anodizing quality, and it is available everywhere. Choose 7075-T6 when you need steel-adjacent strength and can accept higher cost and stress-related distortion risk. Choose 5052 or 5083 for marine and corrosive environments. Choose 6063 when appearance and anodized color matter more than strength. Choose MIC-6 cast plate when flatness after heavy material removal is the requirement. If your drawing follows EN standards, 6082 is the direct counterpart to 6061.
How tight a tolerance can you hold on aluminum?
We hold ±0.005 mm on critical features with dedicated setups and in-process measurement. Our default for untoleranced dimensions is ISO 2768-m. The practical answer is that tolerance should be applied selectively: identify the two or three features that actually control fit and function, tighten those, and leave the rest at general tolerance. That approach delivers a part that works at a fraction of the cost of a uniformly tight drawing.
Will anodizing change my part's dimensions?
Yes, and this is the single most common cause of aluminum parts failing incoming inspection. Anodizing converts the surface rather than adding to it, so roughly half the coating thickness grows outward from the original surface. A 25 µm Type III hard anodize adds around 12 µm per surface, which is about 0.025 mm on a diameter — enough to turn a sliding fit into an interference fit. We either machine to a compensated pre-plate dimension or mask the critical feature, and we confirm which approach you want before machining starts.
Why did my thin-wall aluminum part warp?
Almost always residual stress. Rolled and heat-treated plate carries locked-in stress from quenching; when machining removes most of the mass, that stress rebalances and the part bows — often hours or days after it leaves the machine. Contributing factors include asymmetric material removal, clamping distortion and cutting heat. The fixes are stress-relief annealing before machining, balanced roughing with a finishing allowance, a settling period before the final passes, and vacuum or soft-jaw fixturing that spreads clamping load. We build these steps into the route for any part where flatness or true position is tighter than 0.05 mm.
What is the minimum wall thickness you can machine in aluminum?
0.8 mm is achievable with appropriate fixturing and finishing strategy; 1.5 mm is the thickness we recommend if your design has flexibility. Below about 1 mm the wall deflects under cutting load, which affects both dimensional accuracy and surface finish, and the part becomes sensitive to how it is clamped. Walls under 0.8 mm are possible on small parts with sacrificial supports, but we will discuss the geometry with you before quoting rather than after.
How much does aluminum CNC machining cost?
Cost is driven by machining time far more than material. The main variables are part complexity, number of setups, tolerance tightness, surface finish requirements, quantity and coating. Aluminum itself is inexpensive and cuts fast, which is why it is usually the most cost-effective machinable metal. The most effective way to reduce your price is a design review before release — send us a STEP file and we will identify the cost drivers in your model at no charge.
Do you machine both prototypes and production volumes?
Yes, with no minimum order quantity. We run single prototype parts and repeat production programs above 100,000 pieces in the same facility, which means you do not need to re-qualify a new supplier when a design moves from validation into volume. The process documentation created during prototyping carries forward into the production route.
What quality documentation do you provide with aluminum parts?
Standard shipments include a material certificate identifying alloy, temper and heat lot, plus a dimensional inspection report covering the critical characteristics on your drawing. Full first-article inspection and PPAP documentation are available for production programs. Our facility operates under ISO 9001:2015, and final dimensions are verified on coordinate measuring machines — after surface treatment where a coating is specified.
Send us the part that keeps coming back out of tolerance
Upload a STEP file and a drawing. You will get a price, a lead time and an engineer's assessment of what is likely to move — within two working hours.
Get your aluminum quoteAll uploads confidential · NDA available on request · sales@richconn.com