
CNC Machining a 5052 Aluminum Magnetic Strip with 0.05 mm Flatness Control
Richconn machined a cross-shaped 5052 aluminum magnetic strip for automation equipment. The part had four rib features that were prone to warping and deformation, so the machining process needed to control material stress, thickness allowance, precision hole timing, and final flatness.
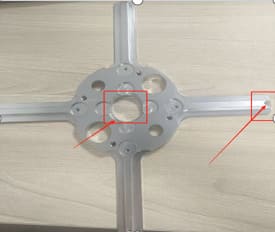
Cross-Shaped Aluminum Part with Four Rib Features and High Deformation Risk
This case involved CNC machining of a 5052 aluminum magnetic strip used in automation equipment. The part had a cross-shaped structure, and the four rib features were likely to warp during machining because of the aluminum material and the structural layout.
The customer needed the final part to remain stable with no visible deformation, while the flatness had to be controlled within 0.05 mm. For this type of precision aluminum part, good equipment alone is not enough. A reasonable process route is critical to controlling deformation.

Technical drawing reference for the 5052 aluminum magnetic strip, showing the cross-shaped structure and rib features that required deformation control during CNC machining.
Why This 5052 Aluminum Magnetic Strip Was Difficult to Machine
The customer’s main problem was deformation. Because the product had a cross-shaped structure with four rib features, the ribs were easy to lift, warp, or deform during machining.
If the deformation was not controlled, the part could not meet the customer’s flatness requirement or support stable precision assembly in automation equipment.
Main Manufacturing Risks
- The four rib features were easy to warp during material removal.
- The 5052 aluminum material and part structure created deformation risk.
- Machining precision holes too early could cause positional deviation after deformation.
- Thickness finishing needed to be controlled after roughing and shape correction.
- The final flatness needed to stay within 0.05 mm.
The Core Difficulty Was Aluminum Deformation Caused by Structure and Machining Stress
The deformation risk came from both material behavior and product structure. The 5052 aluminum part had four rib features arranged in a cross-shaped layout, which made the part sensitive to internal stress release and uneven material removal during CNC machining.
| Material Factor | 5052 aluminum can deform when machining stress and material removal are not properly controlled. |
|---|---|
| Structural Factor | The cross-shaped structure and four rib features increased the tendency for warping and lifting. |
| Process Risk | If precision holes were machined too early, later deformation could affect hole accuracy and assembly alignment. |
| Flatness Requirement | The finished product needed to be free from deformation and maintain flatness within 0.05 mm. |
How We Controlled Warping and Final Flatness
Richconn adjusted the machining route around deformation control. The process used annealing, staged roughing allowance, delayed precision hole machining, and final shape correction before finishing the thickness and precision holes.
5052 Material Annealing
The 5052 aluminum material was annealed first to help reduce internal stress before the main CNC machining operations.
Rough Thickness Machining
During rough machining, Richconn left a 1 mm allowance on thickness to prevent the part from being brought to final size too early.
Delay Precision Hole Machining
The precision holes were not machined in the first stage. Other dimensions were processed first while leaving the critical holes for later finishing.
Shape Correction and Final Finishing
After shape correction, the thickness was finished to final size, and the precision holes were then machined to the required dimensions.
mm flatness achieved within the customer’s requirement
after annealing, staged allowance control, shape correction, and final precision hole machining
No Deformation and Flatness Controlled Within 0.05 mm
After process optimization, the finished magnetic strip had no deformation, and the flatness was controlled within 0.05 mm. The final result met the customer’s requirement for the automation equipment application.
- Material: 5052 aluminum
- Process: CNC machining
- Quantity: 8 pieces
- Key issue: four rib features prone to warping
- Process control: annealing, 1 mm rough allowance, delayed precision hole machining
- Final result: no deformation
- Flatness achieved: within 0.05 mm
What Buyers Should Know About CNC Machining Deformation-Sensitive Aluminum Parts
For high-precision aluminum parts, machining accuracy depends not only on equipment capability, but also on the process route. When a part has ribs, thin areas, cross-shaped structures, or asymmetric material removal, deformation control should be planned before machining begins.
In this case, annealing, staged allowance, delayed precision hole machining, and final shape correction helped the part reach the required flatness without deformation.
Richconn’s Practical Experience
- Use annealing when aluminum stress release may affect final flatness.
- Leave enough roughing allowance before final thickness finishing.
- Avoid machining precision holes too early on deformation-sensitive parts.
- Use shape correction before final finishing operations.
- Plan the machining process around the part structure, not only around the drawing dimensions.
Related CNC Machining Services
Richconn supports custom CNC machining of aluminum parts, automation equipment components, deformation-sensitive structural parts, precision plates, magnetic strip components, brackets, and custom machined parts based on customer drawings.
FAQ About 5052 Aluminum CNC Machining and Flatness Control
Why do 5052 aluminum parts deform during CNC machining?
5052 aluminum parts can deform because of internal stress release, uneven material removal, thin or ribbed structures, and unsuitable machining sequence.
How can flatness be controlled on ribbed aluminum parts?
Flatness can be controlled by annealing the material, leaving enough roughing allowance, machining in stages, correcting the shape before final finishing, and delaying precision hole machining until the part is stable.
Why were the precision holes machined later?
If precision holes are machined before the part shape becomes stable, later deformation may affect hole position and assembly accuracy. Machining precision holes after shape correction helps protect final dimensional accuracy.
Can Richconn machine similar deformation-sensitive aluminum parts?
Yes. Richconn can support CNC machining of deformation-sensitive aluminum parts, ribbed structures, precision plates, automation equipment parts, and custom components requiring flatness and hole accuracy control.
Need a 5052 Aluminum Part Machined with Flatness Control?
Send us your 2D drawings, 3D files, material requirements, flatness tolerance, hole tolerance, structure details, and quantity. Richconn’s engineering team will review the deformation risk and provide a practical CNC machining solution.