
Turn-Mill Machining an AISI 630 Flanged Handwheel with Smooth M14×1.5 Thread
Richconn machined an AISI 630 flanged handwheel for automation equipment. The customer needed smooth M14×1.5 thread performance and a clean appearance on the arc area. The project required process sequence control, optimized arc machining parameters, and final polishing to remove chatter marks.
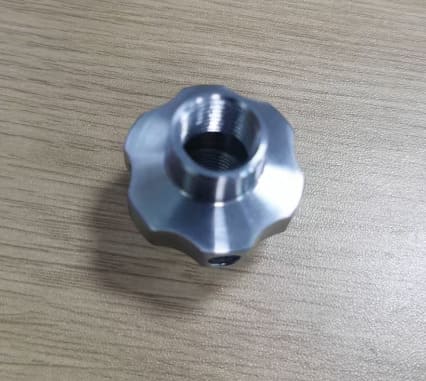
Flanged Handwheel Requiring Smooth Thread Assembly and Appearance Surface Control
This case involved turn-mill machining of a flanged handwheel made from AISI 630 for automation equipment. The part included an M14×1.5 fine thread and visible arc surfaces, so both assembly function and appearance quality needed to be controlled.
The customer’s main issue was that the M14×1.5 thread was not smooth after machining, and the arc area showed obvious chatter marks. Because the part was an appearance component, surface smoothness and thread usability were both important for final acceptance.

Technical drawing reference for the AISI 630 flanged handwheel, showing the M14×1.5 thread, side hole, and six-angle arc area.
Why the M14×1.5 Thread Was Not Smooth After Machining
The customer reported that the M14×1.5 thread was not smooth during use. In addition, the visible arc area of the handwheel had obvious chatter marks, which affected the appearance of the part.
The thread was a fine thread, and side drilling after thread machining caused burrs or raised edges near the hole opening. This affected thread smoothness and made assembly or operation less reliable.
Main Manufacturing Risks
- M14×1.5 fine thread required clean cutting and smooth engagement.
- Side drilling after thread machining could create burrs and raised edges at the hole opening.
- Burrs near the thread could make the thread feel rough or unsmooth.
- The six-angle arc surface was prone to chatter marks during CNC machining.
- As an appearance part, the visible arc area needed a smooth final finish.
The Core Difficulty Was Process Sequence and Chatter Control on the Appearance Arc
The problem came from two areas: thread process sequence and arc surface machining stability. When the side hole was drilled after the M14×1.5 thread, material at the hole opening could deform or create burrs, making the thread feel unsmooth. At the same time, arc machining generated chatter marks that reduced appearance quality.
| Thread Smoothness Risk | The M14×1.5 fine thread needed smooth engagement, but burrs from side drilling could interfere with thread performance. |
|---|---|
| Process Sequence Risk | Machining the side hole after the thread increased the chance of burrs or raised edges affecting the thread. |
| Arc Surface Risk | The visible six-angle arc area was prone to chatter marks during CNC machining. |
| Appearance Requirement | The handwheel was an appearance component, so final smoothness and polished arc quality were important. |
How We Improved Thread Smoothness and Arc Appearance
Richconn changed the machining sequence and used turn-mill machining to control both thread function and appearance quality. The side hole was completed first, then the M14×1.5 thread was machined. The six-angle arc area was machined using controlled CNC parameters, followed by manual polishing.
Turn-Mill Process Selection
Turn-mill machining was selected to handle the handwheel’s turning, side-hole, thread, and arc features in a controlled process route.
Side Hole Before Threading
The side hole was drilled to final condition first, and the M14×1.5 thread was machined afterward to avoid burrs affecting thread smoothness.
Controlled Arc Machining Parameters
The six-angle arc was machined on the CNC with feed 300, cutting amount 0.2, and spindle speed 1500 to reduce chatter marks.
Manual Arc Polishing
The arc area was manually polished and deburred to ensure a smooth appearance surface and better hand feel.
pieces completed with smooth thread and surface finish
thread became smooth after adjusting process sequence and controlling burrs

Smooth Surface and Smooth M14×1.5 Thread Achieved
After the process was optimized, the product surface became smooth, the M14×1.5 thread operated smoothly, and the finished handwheels met the customer’s assembly and use requirements.
- Material: AISI 630
- Process: turn-mill machining
- Quantity: 70 pieces
- Key feature: M14×1.5 fine thread
- Main issue: unsmooth thread and chatter marks on the appearance arc
- Process control: side hole first, thread afterward, optimized arc cutting parameters
- Final result: smooth surface and smooth thread
What Buyers Should Know About Turn-Mill Machining for Threaded Appearance Parts
For threaded appearance parts, machining quality is not only about dimensional accuracy. Thread smoothness, burr control, process order, surface texture, and final polishing all affect whether the part can be assembled and used comfortably.
In this case, changing the side-hole and threading sequence, reducing chatter on the arc surface, and manually polishing the visible area helped the handwheel meet both functional and appearance requirements.
Richconn’s Practical Experience
- Plan side-hole drilling and threading order carefully when they intersect or influence each other.
- Control burrs near fine threads to protect smooth assembly and operation.
- Adjust feed, cutting amount, and spindle speed when arc surfaces show chatter marks.
- Use manual polishing when an appearance arc requires a smooth final finish.
- Evaluate threaded parts by both measurement and real assembly or hand-feel feedback.
Related CNC Machining Services
Richconn supports turn-mill machining of threaded parts, handwheels, knobs, shaft-fitting parts, automation equipment components, and appearance metal parts requiring burr control, surface finish, and assembly performance.
FAQ About AISI 630 Turn-Mill Machining and Thread Smoothness
Why can an M14×1.5 thread become unsmooth after machining?
Fine threads can become unsmooth when burrs, raised edges, or deformation appear near the thread. In this case, drilling the side hole after threading caused burrs at the hole opening, which affected thread smoothness.
Why was the side hole machined before the thread?
Machining the side hole first reduced the risk of burrs damaging or interfering with the finished M14×1.5 thread. The thread was then machined afterward to restore smooth engagement.
How were chatter marks reduced on the arc surface?
The six-angle arc was machined using controlled CNC parameters, including feed 300, cutting amount 0.2, and spindle speed 1500, followed by manual polishing of the arc area.
Can Richconn machine similar threaded appearance parts?
Yes. Richconn can support turn-mill machining of threaded components, handwheels, knobs, automation equipment parts, and appearance parts requiring smooth surfaces and reliable assembly performance.
Need a Threaded Appearance Part Machined with Smooth Assembly?
Send us your 2D drawings, 3D files, material requirements, thread specifications, side-hole details, surface finish requirements, appearance areas, and quantity. Richconn’s engineering team will review the process risks and provide a practical machining solution.