
Turn-Mill Machining a 1.2210 Steel Concentric Shaft with 0.02 mm Concentricity
Richconn machined a 1.2210 steel concentric shaft for automation equipment. The customer required 0.02 mm concentricity and 0.01 mm circular runout, but the original process could not keep the inner hole and outer diameter aligned reliably. Richconn solved the issue through customized tooling, controlled turning allowance, precision grinding, and full CMM inspection.
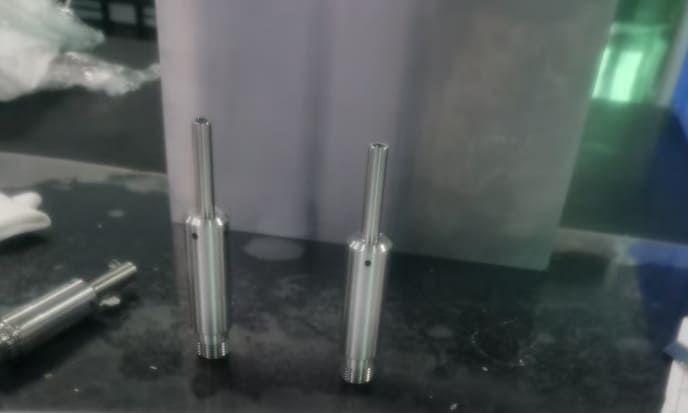
Concentric Shaft Requiring Inner and Outer Diameter Alignment
This case involved turn-mill machining of a concentric shaft made from 1.2210 steel for automation equipment. The component required strict control of concentricity and circular runout, because the part needed to match the customer’s assembly and use requirements.
The customer’s required concentricity was 0.02 mm, and the circular runout requirement was 0.01 mm. For shaft parts with both inner hole and outer diameter requirements, tool deflection, tool setting error, and process sequence can directly affect coaxial accuracy.

Technical drawing reference for the 1.2210 steel concentric shaft, showing the inner hole, outer diameter, and concentric shaft structure.
Why the 0.02 mm Concentricity and 0.01 mm Runout Could Not Be Guaranteed
The customer needed the concentric shaft to meet 0.02 mm concentricity and 0.01 mm circular runout. However, the original machining process could not guarantee these requirements consistently.
The key issue was that the outer diameter and inner hole were not machined by the same tool setup. Tool swing and tool setting deviation introduced alignment error between the inner and outer features.
Main Manufacturing Risks
- 0.02 mm concentricity required stable alignment between the inner hole and outer diameter.
- 0.01 mm circular runout left very little room for tool setting or machining deviation.
- Different tool setups for inner and outer features increased accumulated error.
- Tool swing could affect coaxial accuracy during machining.
- The final part needed to pass customer assembly fit, not only dimensional inspection.
The Core Difficulty Was Alignment Error Between Inner Hole and Outer Diameter
The root cause was that the outer diameter and inner hole were not completed in one stable machining relationship. When different tools or different setups are used, tool runout, tool setting deviation, and datum transfer error can cause concentricity and circular runout to drift beyond tolerance.
| Concentricity Requirement | The customer required 0.02 mm concentricity between the shaft features. |
|---|---|
| Circular Runout Requirement | The circular runout requirement was 0.01 mm, requiring stable rotational accuracy. |
| Process Error Source | The inner hole and outer diameter were not machined in the same tool relationship, creating accumulated alignment error. |
| Tooling Risk | Tool swing and tool setting error affected the accuracy between the inner and outer cylindrical features. |
How We Controlled Concentricity and Circular Runout
Richconn optimized the process route around coaxial accuracy. The solution used customized long tooling, controlled turning allowance, inner and outer cylindrical grinding, precision grinding to final dimensions, and full CMM inspection.
Customized Long Tooling
A customized extended tool was prepared to support the machining requirements of the concentric shaft and reduce process instability.
Turning with 0.2 mm Allowance
The turning process was controlled with a 0.2 mm allowance, leaving material for the subsequent precision grinding stage.
Inner and Outer Cylindrical Grinding
The inner and outer cylindrical features were ground to improve coaxial accuracy and bring the critical dimensions to final size.
Full CMM Inspection
Each part was fully inspected by CMM to verify concentricity, circular runout, and dimensional stability before delivery.
mm circular runout requirement achieved after process optimization
concentricity requirement achieved with no deviation and customer assembly fit passed
Concentricity and Circular Runout Met the Customer’s Assembly Requirement
After the process was optimized, the concentricity and circular runout showed no deviation. The customer’s real assembly fit requirement was satisfied.
- Material: 1.2210 steel
- Process: turn-mill machining with precision grinding
- Quantity: 3 pieces
- Customer concentricity requirement: 0.02 mm
- Customer circular runout requirement: 0.01 mm
- Process control: customized long tool, 0.2 mm turning allowance, inner and outer cylindrical grinding
- Inspection: full CMM inspection
- Final result: no deviation in concentricity or circular runout, customer assembly fit passed
What Buyers Should Know About Concentric Shaft Machining
For concentric shafts, machining quality depends on the relationship between the inner hole, outer diameter, datum control, tooling rigidity, and final inspection. Even when individual dimensions appear correct, poor alignment between inner and outer cylindrical features can cause runout and assembly problems.
In this case, controlled allowance, grinding of inner and outer cylindrical features, and full CMM inspection helped ensure the shaft matched the customer’s assembly and use requirements.
Richconn’s Practical Experience
- Control the machining relationship between inner holes and outer diameters early in process planning.
- Use controlled turning allowance before final precision grinding.
- Reduce tool swing and tool setting deviation when coaxial accuracy is critical.
- Use inner and outer cylindrical grinding for tight concentricity and runout requirements.
- Verify critical shaft parts with CMM inspection before delivery.
Related CNC Machining Services
Richconn supports turn-mill machining of concentric shafts, precision shaft parts, automation equipment components, inner and outer cylindrical parts, and custom metal components requiring concentricity, circular runout, grinding, and CMM inspection.
FAQ About Concentric Shaft Machining and Runout Control
Why is concentricity difficult to control on shaft parts?
Concentricity is difficult to control when the inner hole and outer diameter are machined in different setups or with different tool relationships. Tool setting error, datum transfer, and tool swing can create alignment deviation between the features.
Why was 0.2 mm turning allowance left before grinding?
Leaving 0.2 mm allowance gives enough material for precision grinding, allowing the critical inner and outer cylindrical features to be finished more accurately.
How can circular runout be controlled on concentric shafts?
Circular runout can be controlled through stable datum planning, reduced tool swing, controlled turning allowance, cylindrical grinding, and final inspection using CMM or other precision measuring methods.
Can Richconn machine similar precision shaft components?
Yes. Richconn can support turn-mill machining, CNC turning, grinding, and inspection of concentric shafts, precision shaft parts, automation equipment components, and custom parts requiring tight concentricity and runout control.
Need a Precision Shaft Machined with Concentricity and Runout Control?
Send us your 2D drawings, 3D files, material requirements, concentricity tolerance, runout tolerance, grinding requirements, inspection requirements, and quantity. Richconn’s engineering team will review the machining and inspection risks and provide a practical process solution.