
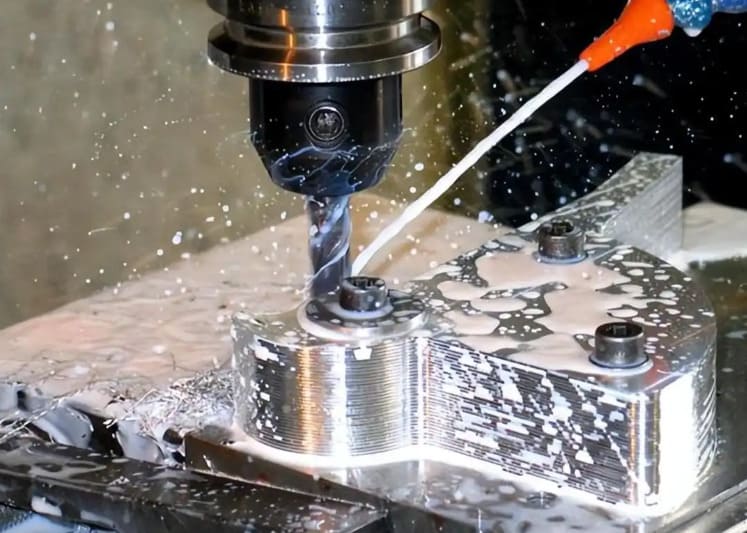
Three things that go wrong on stainless — and what we do about each
Stainless has a machinability rating between 25% and 45% of free-machining steel, but the number is not really the problem. The problem is that stainless fails suddenly rather than gradually: a process that works for ninety parts destroys the ninety-first.
The skin gets harder than the part
Austenitic grades like 304 and 316 harden dramatically under deformation. A dull edge, a dwell at the bottom of a hole, or a finishing pass too light to form a chip all rub instead of cut — leaving a hardened layer that the next tool has to break through.
The heat stays in the cutting zone
Stainless conducts heat about a third as well as carbon steel, so the energy that aluminum carries away in its chips stays at the tool tip. The result is rapid flank wear, notching at the depth-of-cut line, and thermal growth that drifts the part out of tolerance mid-run.
Threads seize, chips wrap
Stainless is ductile and self-welding. Threads gall during forming and again during assembly; austenitic grades throw long stringy chips that wrap the tool and score a finished bore on the way out.
The grades we machine, ranked by what they cost you in cycle time
Corrosion resistance and machinability pull in opposite directions in stainless. The grade that survives your environment best is usually the one that is hardest to cut — so the choice is a real trade-off, not a default. Machinability ratings below are relative to free-machining B1112 steel at 100%.
| Grade | Family | Machinability | Behavior in the cut | Specify it when |
|---|---|---|---|---|
| 303 | Austenitic | ~78% | The easy one. Added sulphur breaks chips cleanly and cuts cycle time sharply against 304. | You need corrosion resistance and volume, and the part is not welded or exposed to chlorides |
| 304 / 304L | Austenitic | ~45% | Work-hardens fast, throws long chips, needs rigidity. The industry default and the benchmark for cost. | General-purpose corrosion resistance, food contact, welded assemblies (304L) |
| 316 / 316L | Austenitic | ~36% | Everything 304 does, harder. Molybdenum raises toughness and heat retention — expect longer cycles and higher tooling cost. | Saltwater, chlorides, pharmaceutical or surgical use where pitting resistance is required |
| 321 | Austenitic | ~36% | Similar to 304 with titanium stabilisation; tougher, stringier chips. | Parts welded and then exposed to 425–870 °C service |
| 416 | Martensitic | ~90% | The most machinable stainless available. Excellent for high-volume turned parts, but the weakest corrosion resistance in the group. | Shafts, studs and fittings in dry or mildly corrosive service, at volume |
| 420 | Martensitic | ~45% (annealed) | Machined annealed, then hardened. Plan the heat-treat distortion allowance before finishing. | Cutting edges, moulds, wear surfaces needing hardness plus some corrosion resistance |
| 440C | Martensitic | ~40% (annealed) | High carbon and abrasive; tool wear is the constraint. Grinding after hardening is often the only route to tight tolerance. | Bearings, valve seats, high-hardness wear components |
| 17-4PH | Precipitation hardening | ~48% (Cond. A) | Machined in Condition A, then age-hardened to H900–H1150. Ageing shrinks the part slightly and predictably — the condition must be on the drawing. | High strength plus corrosion resistance: aerospace fittings, valve and pump shafts, surgical instruments |
| 15-5PH | Precipitation hardening | ~48% (Cond. A) | Comparable to 17-4PH with better transverse toughness; same heat-treat planning applies. | Aerospace structure where directional toughness matters |
| 2205 duplex | Duplex | ~25–30% | The hardest of the group to cut: high strength, high work hardening, aggressive on edges. Budget significantly longer cycles. | Offshore, chemical and desalination service where 316 will still pit |
Unsure between 304 and 316? The cost difference in machining is often larger than the material difference. Send the service environment and we will tell you whether 316 is buying you anything. Background reading: stainless steel types and grades explained.
Rigidity decides the route
On stainless, machine choice matters more than it does on aluminum. Deflection that would cost you 0.01 mm in aluminum costs you a work-hardened surface and a broken tool here.

CNC milling
Manifolds, housings, flanges and brackets. High-torque spindles and short tool reach for stable cutting in 304 and 316.

5-axis machining
Complex geometry in one clamping. Fewer setups means fewer re-entries into a work-hardened surface — a real quality gain, not just a time saving.

CNC turning
Shafts, valve bodies, fittings and precision bushings. Live tooling completes cross-features without a second setup.

Turn-mill machining
Turned and milled features in one clamping, holding concentricity that a two-machine route would lose to re-fixturing.

Swiss stainless machining
Small-diameter, long-aspect parts on CITIZEN and TSUGAMI machines — surgical pins, contacts, micro shafts to ±0.001 mm.

Wire EDM
Sharp internal corners and hardened 440C or aged 17-4PH, where cutting force and tool wear rule out a milling route entirely.
What we hold on stainless
The same tolerance costs more in 316 than in 6061 — not because the machine is less accurate, but because reaching it takes more passes, more tool changes and more in-process measurement. Tolerance selectively, and the price difference narrows considerably.
| Characteristic | Standard (default) | Precision (on request) | Notes |
|---|---|---|---|
| Linear, milled & turned | ISO 2768-m | ±0.01 mm | Applied to untoleranced dimensions unless your title block says otherwise |
| Swiss-turned features | ±0.01 mm | ±0.001 mm | Small-diameter bar work on sliding-headstock machines |
| Hole diameter | H8 | H7 (reamed / bored) | Reaming stainless requires correct pre-drill size — undersize causes rubbing and work hardening |
| Concentricity, turned | 0.05 mm TIR | 0.01 mm TIR | Precision band needs single-setup turn-mill or Swiss machining |
| Surface finish, as-machined | Ra 3.2 µm | Ra 0.8 µm | Ra 0.4 µm and below requires polishing or electropolishing |
| Post-heat-treat, 17-4PH | Per drawing after ageing | Grind to final | State the condition (H900 / H1025 / H1150) — dimensions change during ageing |
Final dimensions verified on coordinate measuring machines. Dimensional reports ship with every order; FAI and PPAP documentation available for production programs.
The corrosion failure that starts in the machine shop
A 316 part can arrive perfectly in tolerance and still rust in service. It usually means free iron was embedded in the surface during machining — from a tool, a fixture, a deburring wheel or a chip from a carbon-steel job on the same table. The oxide layer cannot form over that iron, so it corrodes, and the pit spreads underneath.
This is the single most common stainless complaint we see from buyers switching suppliers, and it is almost never mentioned on a machining service page.
- Segregated tooling and media — deburring and blasting media used on stainless is never shared with carbon steel work
- Passivation to standard — nitric or citric acid per ASTM A967 or AMS 2700, specified on the router, not left to the finisher's discretion
- Electropolishing where a smoother, cleanable surface is required for pharmaceutical or vacuum service
- Ferrite and magnetic permeability — cold work raises permeability in 304 and 316; if your application is MRI, sensor or semiconductor related, tell us and we will plan the route and annealing around it
- Documented cleaning — ultrasonic cleaning before packing on medical and food-contact parts
More detail: our guide to stainless steel passivation.
Finishes for stainless

| Finish | Why specify it |
|---|---|
| As-machined | Ra 1.6–3.2 µm. Lowest cost; tool marks visible |
| Passivation | Removes free iron and restores the oxide layer. Effectively mandatory on medical and food-contact parts |
| Electropolishing | Smooths and brightens, removes the deformed surface layer. Pharmaceutical, vacuum and cleanroom service |
| Bead blasting | Uniform matte texture; use stainless-dedicated media only |
| Polishing | Ra 0.4 µm and below, up to mirror. Sanitary, optical and decorative faces |
| PVD coating | Hard colored finish. Stainless cannot be anodized — PVD is the route to black or gold |
| Black oxide | Matte non-reflective finish for optical and defence assemblies |
| Laser marking | Permanent UDI codes, part numbers and lot traceability |
Machining aluminum too? See our aluminum CNC machining services.
Five decisions that move a stainless quote most
- Check whether you actually need 316. If the part never sees chlorides, 304 machines faster and costs less; if it is a dry indoor fitting at volume, 303 or 416 can halve the cycle time.
- Open internal corners. Small radii force small tools, and small tools in stainless mean light passes, rubbing and short tool life. R3 instead of R1 can change the process entirely.
- Keep deep features shallow. Long-reach tooling loses rigidity, and lost rigidity in stainless produces chatter and a work-hardened surface, not just a poor finish.
- Reconsider very fine and very deep threads. Fine pitches in austenitic stainless gall easily. A coarser thread or a slightly larger diameter is usually cheaper and more reliable in assembly.
- State the heat-treat condition and the finish standard. "17-4PH" without a condition and "passivated" without a standard both mean the parts get made twice.
Send a STEP file and we will return a marked-up DFM report identifying the cost drivers — free, before you commit.
Request a DFM reviewWhat ships with the parts
- Material certificate — grade, heat lot and chemistry from the mill
- Dimensional report — CMM results against your critical characteristics
- Passivation certificate — process, standard and test method where specified
- Heat treatment record — condition and process data for PH and martensitic grades
- FAI / PPAP — full first-article documentation on request for production programs
- Traceability — lot-level records retained under our ISO 9001:2015 system

| Stage | Quantity | Typical lead time |
|---|---|---|
| Prototype | 1–10 | 7–12 days |
| Bridge / pilot | 10–500 | 12–25 days |
| Production | 500–100,000+ | Scheduled release |
Stainless lead times run slightly longer than aluminum — heat treatment, passivation and electropolishing are outside operations. Confirmed with your quotation. No MOQ.
Stainless parts we machine every week

Medical & surgical
316L and 17-4PH instruments and device components with passivation certification and UDI marking.
Instrument shafts · housings · pins
Aerospace & defence
17-4PH and 15-5PH fittings and fasteners with full heat-treat and material traceability.
Fittings · brackets · valve bodies
Food & pharmaceutical
304L and 316L contact parts finished to a cleanable surface and documented against your validation requirements.
Nozzles · manifolds · sanitary fittings
Industrial & fluid power
Valve bodies, pump components and precision shafts in 303, 316 and duplex.
Valve bodies · shafts · flanges
Marine & offshore
316 and 2205 duplex hardware for saltwater service, where pitting resistance decides the grade.
Fittings · fasteners · housings
Semiconductor
Low-permeability and vacuum-compatible components with controlled surface preparation.
Probe components · chamber hardwareStainless steel CNC machining questions
Should I specify 304 or 316 stainless steel?
Choose 316 when the part sees saltwater, chlorides or acids — the molybdenum content resists the pitting corrosion that attacks 304 in those environments. Choose 304 for general-purpose corrosion resistance indoors, in fresh water or in food service. The cost difference is not only the material: 316 has a machinability rating around 36% against 45% for 304, so cycle times and tooling costs rise as well. If your part will never see chlorides, specifying 316 adds cost without adding function.
Why is stainless CNC machining more expensive than aluminum?
Almost entirely machining time. Stainless requires lower cutting speeds, absorbs more heat at the tool tip and wears tooling far faster, so the same geometry takes several times longer to cut than in aluminum and consumes more inserts along the way. Work hardening also means more conservative passes and more in-process inspection. Material cost is a secondary factor. The most effective way to reduce a stainless quote is to review the geometry and the grade before release rather than negotiating the price afterwards.
What tolerances can you hold on stainless steel parts?
±0.01 mm on milled and turned features, and down to ±0.001 mm on Swiss-turned small-diameter work. Untoleranced dimensions default to ISO 2768-m. On stainless in particular we recommend tolerancing only the features that control fit and function — holding a tight band on every dimension multiplies inspection time as well as machining time.
What is work hardening and how does it affect my parts?
Austenitic stainless grades harden when deformed. If a cutting edge rubs rather than cuts — because it is dull, because the pass is too light to form a chip, or because the tool dwells — the surface it passes over becomes significantly harder than the parent material. The next tool then has to cut through that layer, which accelerates wear and can break small tools outright. In practice it means stainless is machined with deliberate, consistent chip loads and tooling replaced on schedule rather than run to failure.
Do stainless steel parts need passivation?
In most cases yes, and for medical, pharmaceutical and food-contact parts it is effectively mandatory. Machining embeds free iron from tooling and fixtures into the surface, and the passive chromium oxide layer cannot form over it — so a part that is dimensionally perfect can still rust in service. Passivation to ASTM A967 or AMS 2700 removes that iron and restores the oxide layer. Specify the standard and test method on the drawing rather than writing "passivate" alone.
Can stainless steel be anodized or colored?
No — anodizing applies to non-ferrous metals such as aluminum and titanium. For colored stainless we use PVD coating, which produces a hard metallic finish in black, gold and similar tones, or black oxide for a matte non-reflective surface. Electropolishing and mechanical polishing are the routes to a bright finish without adding a coating.
How do you handle 17-4PH heat treatment?
17-4PH is machined in Condition A and then age-hardened to the condition your drawing calls for — H900 for maximum strength through H1150 for greater toughness. The part changes dimension slightly during ageing, predictably enough to compensate for, so the condition must appear on the drawing before we quote. Where the post-ageing tolerance is very tight, we finish-grind after heat treatment instead of compensating.
Do you machine prototypes as well as production volumes?
Yes, with no minimum order quantity. Single prototypes and repeat production programs run in the same facility, so a design moving from validation into volume does not require qualifying a new supplier — and the process documentation built during prototyping carries into production.
Tell us the grade, the environment and the tolerance that matters
Upload a STEP file and a drawing. You will get a price, a lead time and an engineer's view on whether your grade choice is costing you money — within two working hours.
Get your stainless quoteAll uploads confidential · NDA available on request · sales@richconn.com